Draft Angle Machining
Tapered flutes machine pre-angled pocket sidewalls directly and reduce step-milling operations.
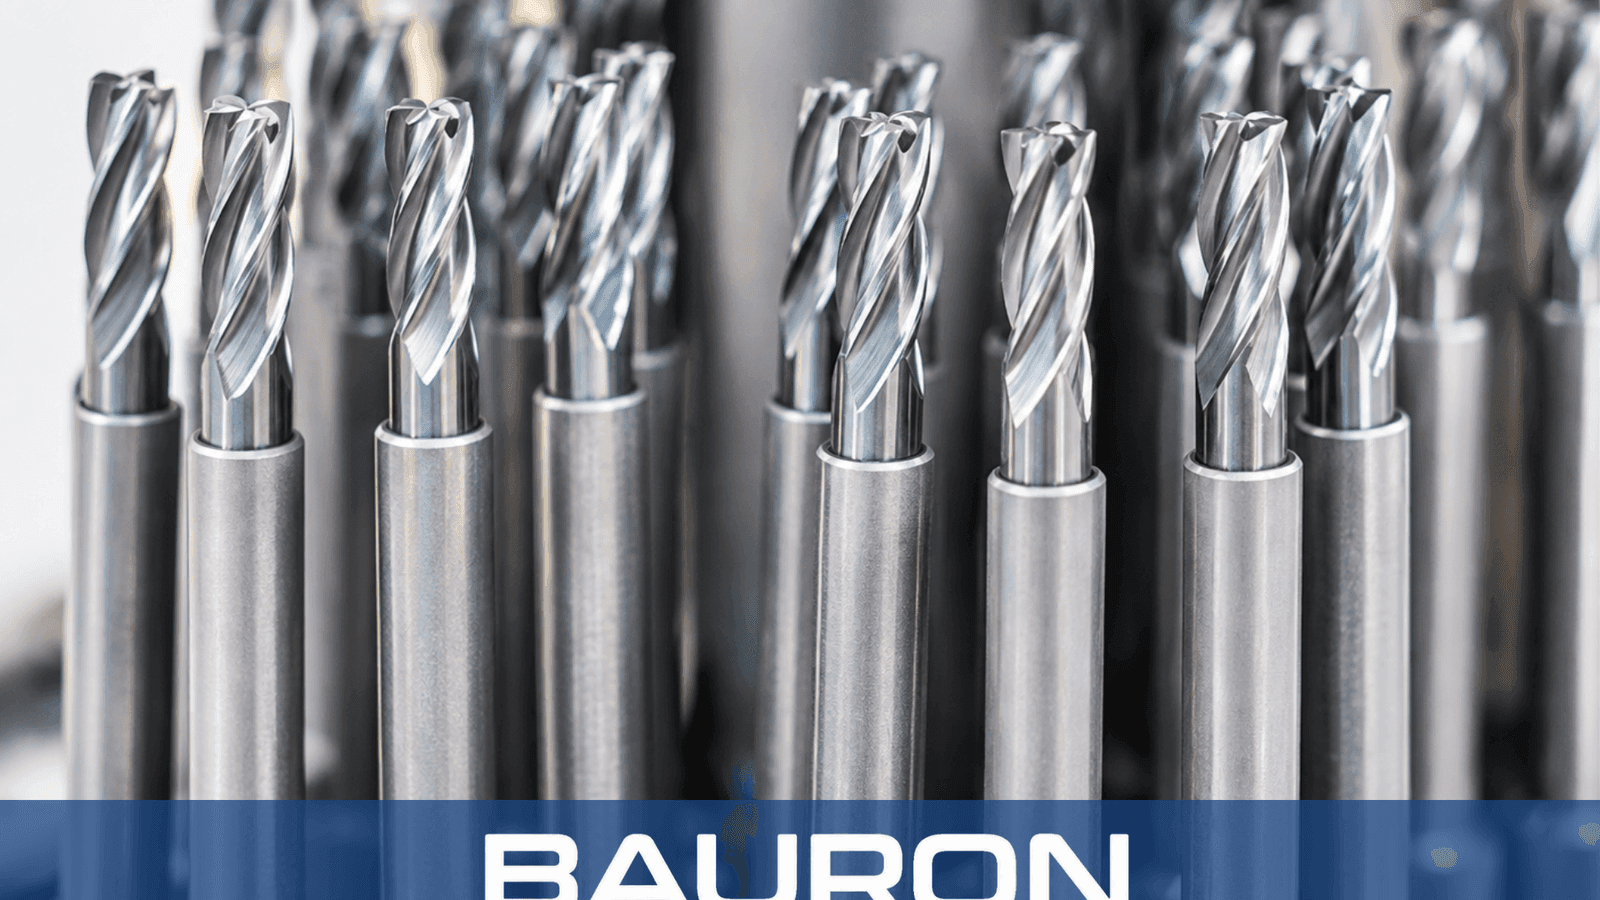
Die sinking cutters, also called tapered ball nose end mills or die sinker end mills, are form cutters for 3D cavity profiling. Their conical core widens from the tip toward the shank so tapered flutes can machine draft walls while the tip profiles cavity floors.
Tapered flutes machine pre-angled pocket sidewalls directly and reduce step-milling operations.
A spherical or corner-radius tip profiles 3D floor transitions and cavity radii.
The conical core thickens toward the shank to resist torsional loads during deep axial cuts.
Helical flutes carry chips upward and out of confined mold cavities.
Cuts draft-angled cavity walls directly and can remove a secondary taper-milling operation.
The conical body helps resist deflection during deep-cavity machining.
Rounded tip profiles support smooth 3D transitions and can reduce manual polishing.
Micro-grain carbide and suitable coatings support cutting in pre-hardened die steels.
Available tip configurations include full ball nose, spherical radius, and flat bottom with corner radius.
| Specification | Range / Details |
|---|---|
| Tip Diameters | 1/16 in to 3/4 in+; metric 1.5 mm to 20 mm+ available |
| Taper Angles per Side | 1°, 1.5°, 2°, 3°, 5°, 7°, 10°, and 15° standard draft angles |
| Tip Profile Options | Full ball nose, spherical radius, or flat bottom with corner radius |
| Flute Count | 2 flutes for roughing or non-ferrous materials; 3 or 4 flutes for finishing hardened steels |
| Shank Style | Straight cylindrical or reinforced tapered shank |
| Operation Type | Deep-cavity roughing, 3D profiling, and die sinking |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| Micro-Grain Solid Carbide | Hardened tool steels including H13, D2, and P20, plus titanium. | Core hardness and stiffness help reduce chatter in deep cavities. |
| nACo / AlTiN Coating | Pre-hardened die steels up to 65 HRC and dry milling. | Oxidation resistance and thermal hardness help protect cutting edges at elevated temperatures. |
| TiSiN / CrN Coating | Abrasive mold materials and non-ferrous alloys. | A hard, low-friction surface helps limit edge wear inside poorly vented pockets. |
Micro-grain carbide provides stiffness for cavity work, nACo or AlTiN supports hardened-steel and dry-milling applications, and TiSiN or CrN addresses abrasive or lower-friction cutting needs.
Run complex 3D toolpaths inside intricate die cavities.
Perform Z-level cavity roughing and 3D surface finishing in mold blocks.
Apply roughing passes to large forging-die blocks.
Sculpts draft-angled cavities in hardened steel forge blocks.
Finishes deep core and cavity features, parting lines, and ribs.
Machines tool-steel dies for automotive stamping and metal extrusion tooling.
Profiles draft-angled passages between complex turbomachinery blades.
Standard ball nose end mills have straight cylindrical bodies. Die sinking cutters use tapered flutes to form a draft angle on the cavity wall while a rounded tip profiles the floor.
Match the cutter taper to the draft angle specified on the mold or die drawing. Plastic injection molds and forging dies commonly call for angles within the listed 1° to 7° range.
Micro-grain carbide cutters with nACo or AlTiN coatings are offered for hardened tool steels such as H13, D2, and S7, with source specifications listing applications up to 65 HRC.
A full ball nose supports continuous 3D floor contouring. A corner-radius tip has a flat center and rounded outer corners for flat-bottomed pockets with radiused transitions.
Bauron can review non-standard taper angles, tip radii, extended-reach clearance necks, and application-specific coatings from mold CAD data.
Bauron provides design and engineering support for custom geometries and coating selections. Share the cavity, material, hardness, tolerances, machine, and production requirements for technical review.
Talk to Engineering